High-efficiency processing machinery engineered for carbonated soft drinks (CSD), sparkling water, and RTD beverage production under humid tropical conditions.
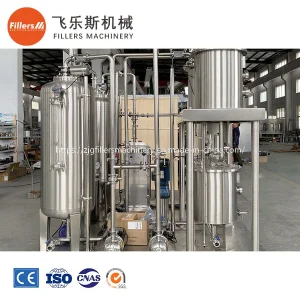
Heavy-duty 6000L/H high-capacity carbonation unit featuring automatic static gas-liquid mixing for medium-to-large bottling operations in Noro.
View Equipment Specs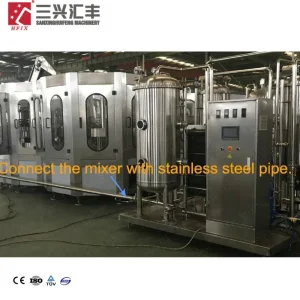
Multi-stage gas-liquid ratio mixing machine optimized for precise CO2 volumes and Brix consistency across varying ambient temperatures.
View Equipment Specs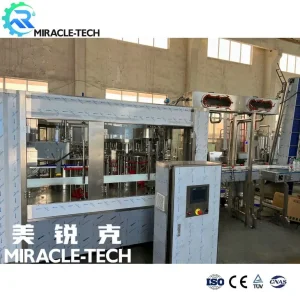
Integrated bottling and carbonation system designed for versatile production of sparkling mineral water, flavored soda, and juices.
View Equipment Specs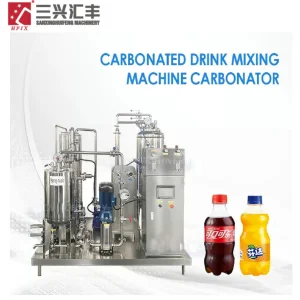
Compact, skid-mounted carbonation unit engineered for small-batch beverage startup plants and regional bottling hubs in Western Province.
View Equipment SpecsAn Engineering Analysis of Carbonation Kinetics, Water Treatment Adaptation, and Operational Optimization in Maritime Tropical Climates
Noro, positioned as the key commercial hub and deep-water port of the Western Province in the Solomon Islands, represents a vital strategic node for food processing and light manufacturing. Known for its established marine exports and agricultural processing infrastructure, Noro is experiencing a rapid diversification in its industrial base. Local demand for packaged, high-quality carbonated beverages, sparkling fruit-infused sodas, and purified carbonated water is expanding significantly across both regional retail channels and hospitality sectors.
However, establishing resilient beverage manufacturing in Noro presents unique engineering challenges. Tropical ambient temperatures regularly exceeding 30°C, high relative atmospheric humidity, maritime salt-air salinity, and potential power grid micro-fluctuations mandate that beverage processing equipment—particularly CO2 mixing and carbonation systems—must be built with robust thermal management, marine-grade anti-corrosion protection (SUS316L/SUS304), and stable PLC-controlled automation.
In carbonated beverage manufacturing, CO2 solubility in water is governed by Henry’s Law, which states that gas solubility decreases as fluid temperature rises. In island processing environments like Noro where municipal water feed temperatures can exceed 26°C, achieved carbonation gas volumes ($GV$) would drop sharply without integrated multi-stage cooling and vacuum degassing.
Our beverage carbonation equipment incorporates advanced vacuum deaeration towers that remove dissolved oxygen down to $< 0.05 \text{ ppm}$. This step prevents oxidation of sensitive beverage flavors, reduces foaming during high-speed bottling, and ensures optimal CO2 bonding within the static mixing injectors at target product temperatures between 2°C and 4°C.
To deliver high Information Gain and practical utility for plant managers, process engineers, and beverage factory owners in Noro, our equipment portfolio incorporates specific technical mechanisms engineered for stability, hygienic integrity, and energy efficiency:
| Technical Metric / Module | Standard Equipment Specification | Engineered Performance Advantage for Noro Plants |
|---|---|---|
| Deaeration Efficiency | Two-stage vacuum spray tower ($<0.05 \text{ ppm } O_2$) | Prevents taste degradation in tropical storage; eliminates neck-space foaming during filling. |
| Syrup-Water Dosing Accuracy | PLC + Mass Flowmeter Ratio System ($\pm 0.05^\circ \text{Brix}$) | Guarantees exact taste profile consistency without manual batching errors or syrup wastage. |
| Carbonation Injection Method | Multi-stage Venturi nozzle + Stainless Static Mixer | Achieves up to 5.0 Vol (GV) CO2 dissolution rate without micro-bubble coalescence. |
| Material & Construction | Full SUS304 / SUS316L Contact Surface, Mirror Polished | Resists marine salt-air corrosion in Noro port district; compliant with FDA & HACCP sanitary standards. |
| Electrical & Controls | Siemens PLC / Schneider Electric with IP65 Enclosure | Protects sensitive micro-controllers from high island humidity and operational washdowns. |
Quantifiable performance metrics defining our high-efficiency processing lines across international trade corridors.
Flexible processing and carbonation configurations tailored to local beverage lines and production scales.
Designed for traditional cola, citrus sodas, energy drinks, and fruit-flavored carbonated beverages. Our 3-component and 4-component mixing systems automatically blend treated water, concentrated syrup, and CO2 gas in continuous stream ratios, delivering continuous high-throughput bottling line feeds.
Equipped with micro-bubble static diffusors that dissolve carbon dioxide into purified reverse-osmosis water at low temperatures, producing smooth bite and crisp mouthfeel desired by resort hotels, retail stores, and commercial dining establishments in Noro and Honiara.
Ideal for local food manufacturers adding specialized beverage lines (e.g., coconut sparkling drinks, tropical fruit fizzy teas). Variable-frequency drives (VFD) allow easy adjustments between low carbonation (2.0 GV) and high carbonation levels (4.2 GV).
Explore our full spectrum of automated mixers, carbonators, batching tanks, and turnkey bottling systems available for direct export to Noro.
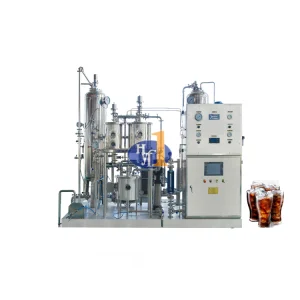
Precision-engineered gas mixing system designed for consistent ratio control and uniform CO2 injection.
View Equipment Specs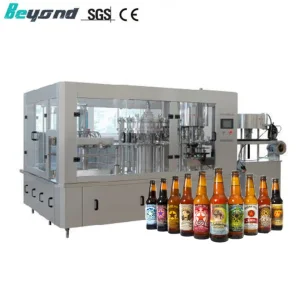
Complete multi-tank mixing and carbonation preparation plant for continuous high-speed soft drink filling lines.
View Equipment Specs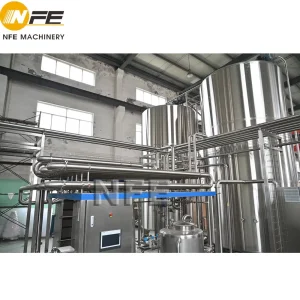
Custom-engineered end-to-end processing plant including batching, thermal flash pasteurization, and carbonation.
View Equipment Specs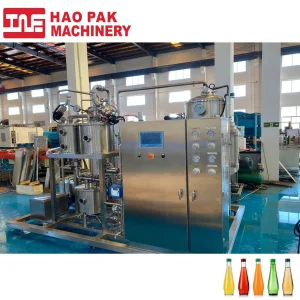
High-pressure carbonation unit optimized for high gas volume beverages such as cola and sparkling tonic water.
View Equipment Specs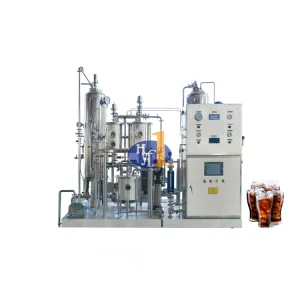
Advanced dual-stage vacuum degassing technology combined with high-precision CO2 mass flow control.
View Equipment Specs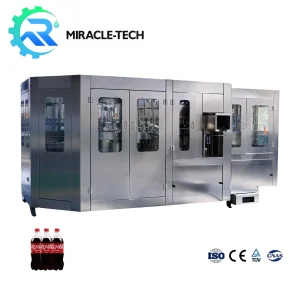
Complete glass/aluminum packaging line with synchronized carbonation dosing, isobaric filling, and capping.
View Equipment Specs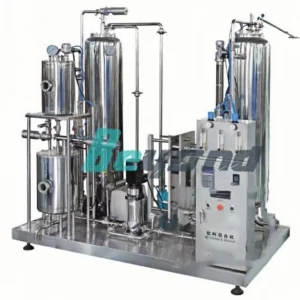
Sanitary food-grade SUS316L construction with automated CIP integration for rapid beverage flavor turnarounds.
View Equipment Specs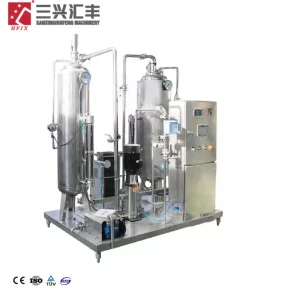
Efficient small-scale processing system tailored for craft sodas and modular production expansion in Western Province.
View Equipment Specs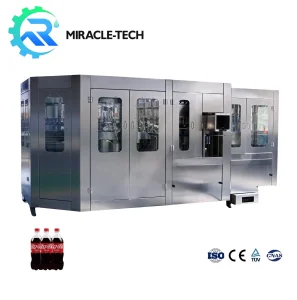
Turnkey solution encompassing water treatment, sugar melting, syrup batching, carbonation, and monoblock filling.
View Equipment Specs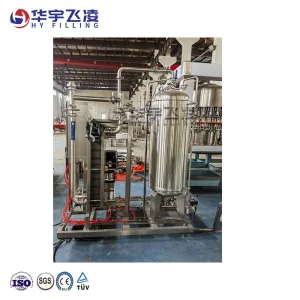
Industrial benchmark carbonator scalable from 3,000L/h up to 20,000L/h for large-scale drink plants serving Noro.
View Equipment Specs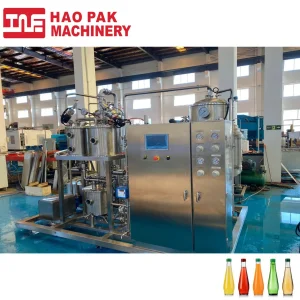
Equipped with high-accuracy static mixing tubes and automated back-pressure regulators for zero gas-loss mixing.
View Equipment Specs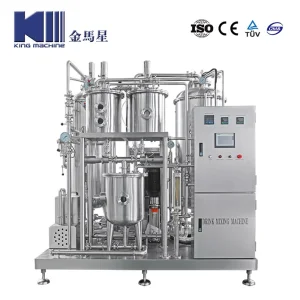
Jacketed stainless steel mixing vessel with integrated carbonation stone diffuser and pressure control manifolds.
View Equipment SpecsEngineering Expertise, Global Quality Compliance, and Turnkey Processing Lines from Dongguan CarniTe Machinery Co., Ltd.
Dongguan CarniTe Machinery Co., Ltd. is a professional manufacturer specializing in fruit and vegetable processing equipment and integrated industrial food processing solutions. The company focuses on the research, development, production, and global supply of advanced processing lines for fruits, vegetables, and related food products. With strong engineering capability and industry experience, CarniTe Machinery delivers turnkey solutions that ensure efficient, hygienic, and scalable food production.
Core systems include washing, sorting, peeling, cutting, juicing, pulping, blanching, freezing, drying, and packaging lines, widely applied in food factories, beverage plants, and agricultural processing industries. The company is committed to improving production efficiency, reducing labor costs, and maintaining consistent product quality through automation and intelligent control technologies.
Dongguan CarniTe Machinery Co., Ltd. maintains strict quality standards and complies with international manufacturing requirements. It provides OEM and ODM customization services tailored to different capacities and production needs.
By combining innovation, reliability, and customer-focused engineering, the company continues expanding into Asia, Europe, the Middle East, and the Americas, aiming to become a trusted global partner in food processing automation.
The company also invests heavily in research and development, continuously upgrading processing technology, improving energy efficiency, and enhancing equipment stability, while providing comprehensive after-sales support, installation guidance, and technical training to ensure long-term operational success for global customers in diverse food manufacturing environments.
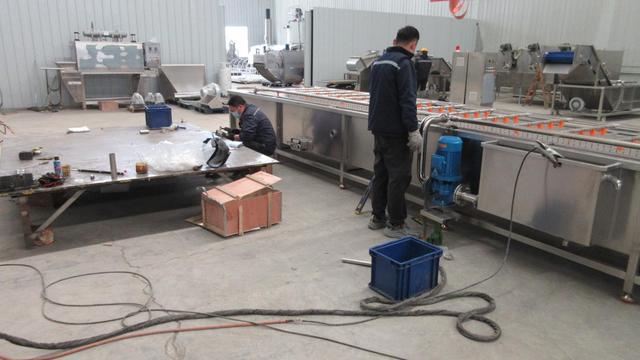
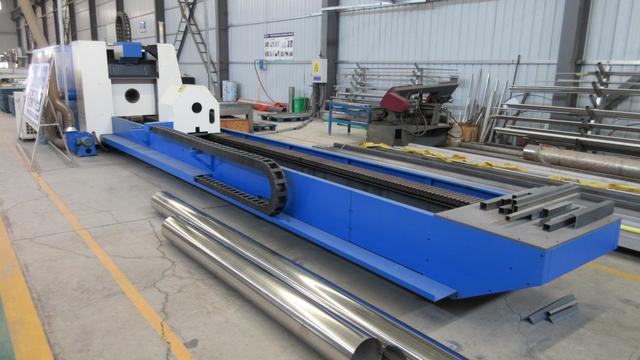
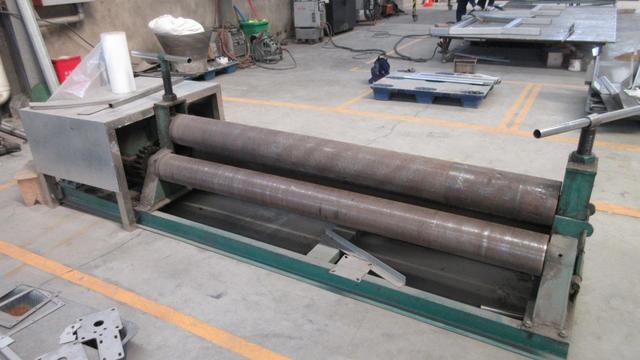
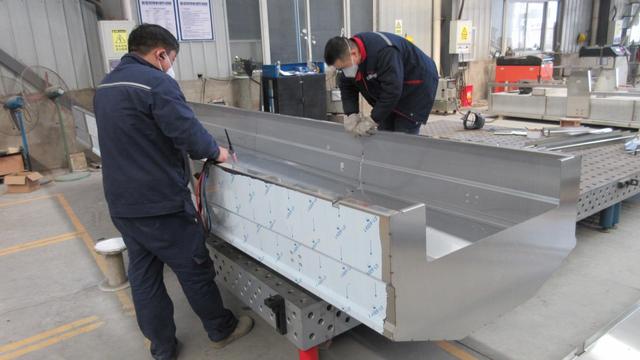
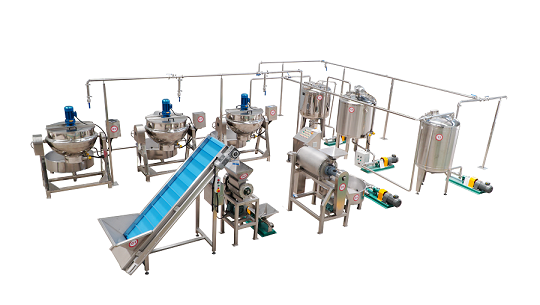
Engineering equipment strictly to global food safety frameworks for seamless operation in Noro and Western Province.
All liquid contact surfaces in our CO2 mixers and batching tanks are constructed from food-grade SUS316L stainless steel, polished to an internal roughness Ra $< 0.4 \mu\text{m}$. Tri-clamp connections prevent bacterial harboring zones during production runs.
Designed with built-in CIP spray balls and automated sanitary valve switching. Systems support high-temperature hot water and chemical wash cycles (caustic soda/acid solution) without requiring manual disassembling of mixer towers.
Carbonation pressure tanks and deaeration columns undergo rigorous hydrostatic testing (1.5x working pressure rating) and carry CE and ASME standard engineering design compliance for high-pressure CO2 processing.
Technical answers to common questions regarding beverage carbonation machinery, logistics, and localized operational setup.
Contact our engineering specialists today for customized equipment quotes, plant layout schematics, and complete technical specifications for carbonation and soft drink processing equipment.
Send Inquiry Now CarniTe Machinery